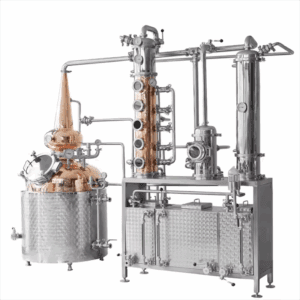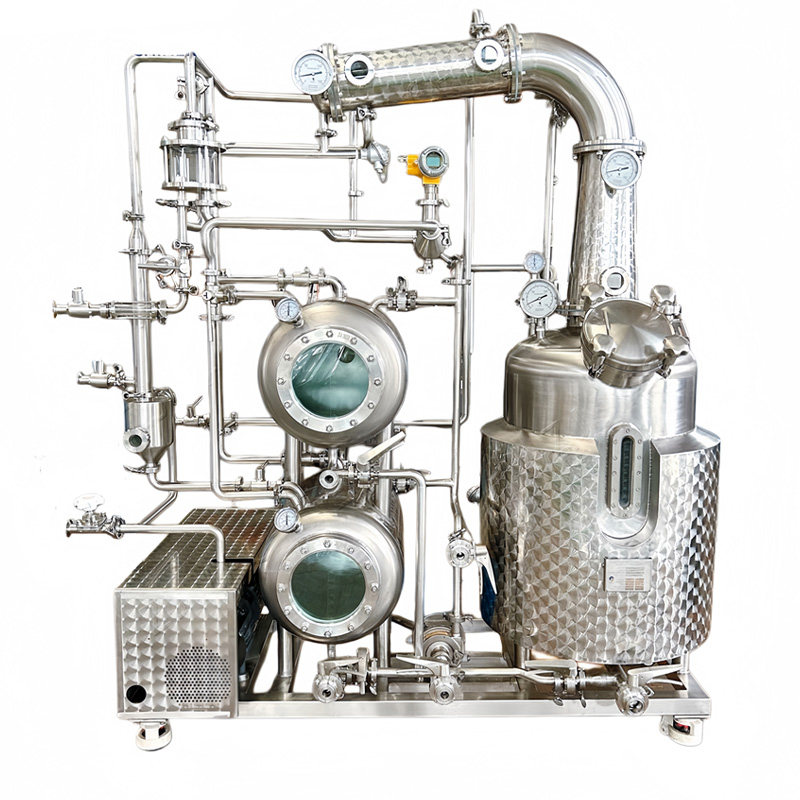
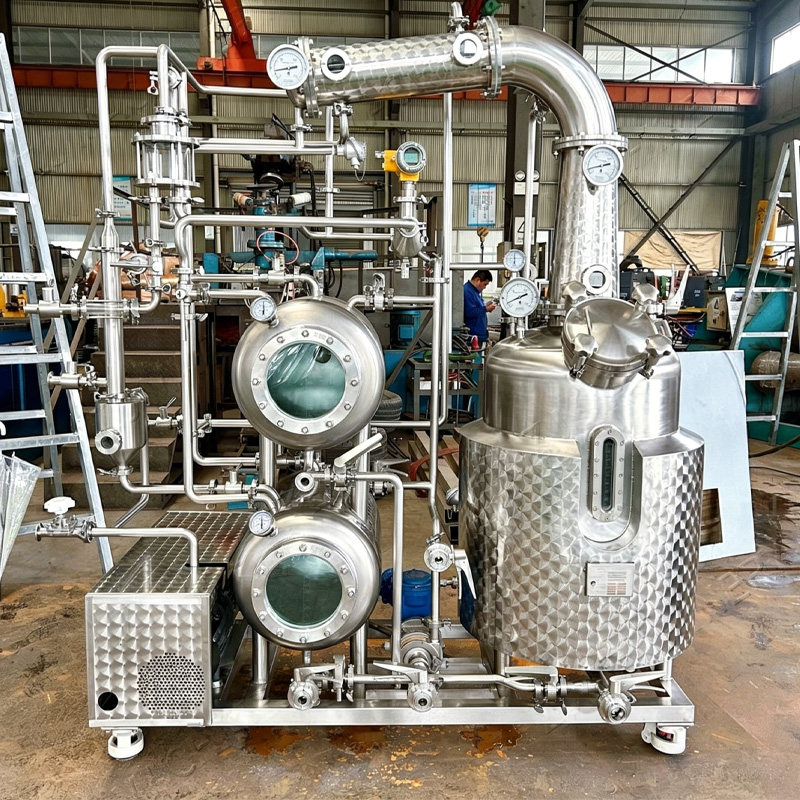
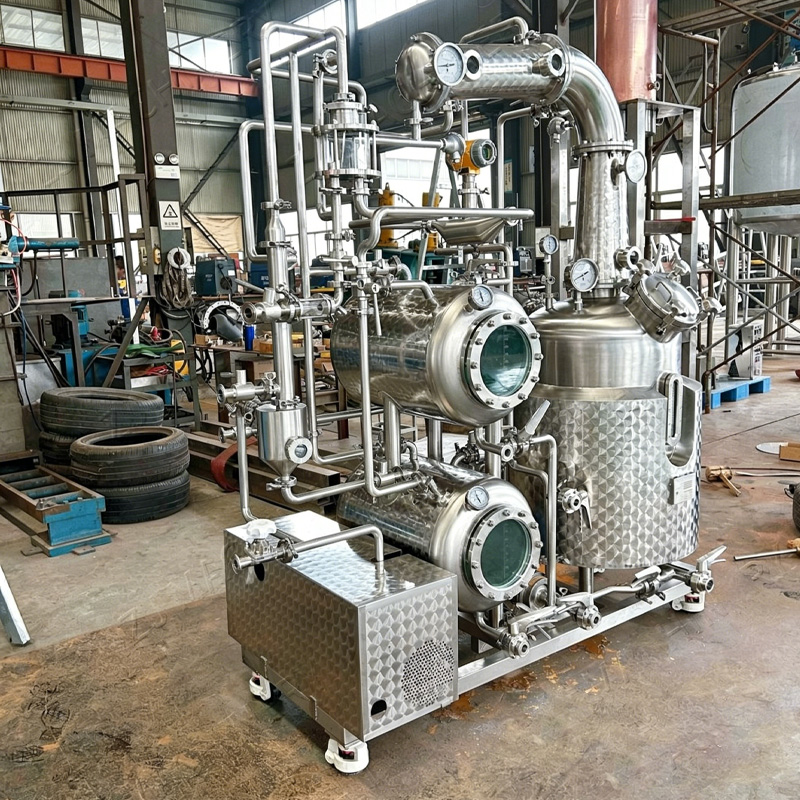
SS304 Double Tank Alcohol Distillation Equipment Manufacturer
SS304 double tank alcohol distillation equipment designed for efficient and continuous alcohol production. The dual-tank system allows alternating operation to reduce downtime and improve productivity. Built with durable stainless steel and optional copper components, it ensures stable performance, high alcohol purity, and consistent output, making it ideal for craft and commercial distilleries seeking scalable and cost-effective production solutions.
Compare
Alcohol Distillation Equipment Product Introduction
The SS304 Double Tank Alcohol Distillation Equipment Manufacturer provides an advanced distillation solution designed for distilleries and alcohol production facilities seeking higher efficiency, continuous operation capability, and stable product quality. This innovative double tank alcohol distillation equipment integrates two independent or interconnected distillation vessels, allowing flexible operation modes such as parallel processing, alternating cycles, or staged distillation.
Compared with traditional single-tank systems, this double tank distillation equipment significantly improves production efficiency by reducing downtime between batches and enabling continuous or semi-continuous operation. One tank can be in the heating or distillation stage while the other is being filled, cleaned, or prepared for the next cycle, maximizing equipment utilization.
Manufactured with high-grade SS304 stainless steel, the system ensures excellent corrosion resistance, hygienic performance, and long service life. The design also supports optional copper components to enhance flavor and remove sulfur compounds when producing high-quality spirits such as whiskey, rum, gin, and vodka.
Industry Pain Points
• Single-tank systems require downtime between batches, reducing overall production efficiency.
• Inconsistent production output due to interruptions in distillation cycles.
• Limited capacity expansion without investing in additional equipment.
• High labor intensity due to manual batch switching.
• Inefficient utilization of heating and cooling systems.
Our Solution
• This double tank alcohol distillation equipment allows alternating operation, minimizing downtime and increasing throughput.
• Parallel processing capability improves production efficiency for commercial distilleries.
• Stable temperature and process control ensure consistent alcohol quality.
• Modular design supports scalability and customization.
• Energy-efficient heat utilization reduces operational costs.
System Overview
• Dual-vessel distillation equipment system designed for continuous and flexible operation.
• Each tank can operate independently or in coordination.
• Includes distillation tanks, condenser system, and control unit.
• Supports batch and semi-continuous distillation processes.
• Easily integrated into full alcohol production lines.
Distillation Process Description
• Fermented mash is loaded into the first tank for distillation.
• While the first tank is distilling, the second tank is prepared for the next batch.
• Vapor is generated through controlled heating and directed to the condenser.
• Distilled alcohol is collected and processed to the required purity.
• Tanks alternate operation, ensuring continuous production flow.
• Optional staged distillation improves alcohol purity and flavor.
Why Choose Double Tank Distillation System
• Increased production efficiency compared to single-tank systems.
• Reduced downtime and higher equipment utilization.
• Flexible operation modes for different production needs.
• Ideal for scaling distillery production.
• Lower operational cost per unit of output.
Technical Specifications
| Item | Specification |
|---|---|
| Product name | SS304 Double Tank Alcohol Distillation Equipment Manufacturer |
| Capacity range | 50L – 1000L per tank (customizable) |
| Material | SS304 stainless steel |
| Structure type | Double tank distillation system |
| Distillation method | Batch / Semi-continuous |
| Heating method | Electric / Steam / Gas |
| Heating power | 6 – 120 kW |
| Cooling system | Water cooling |
| Cooling water flow | 2 – 15 m³/h |
| Alcohol output | 40% – 95% ABV |
| Control system | Manual / Semi-auto / PLC |
| Pressure system | Atmospheric |
| Insulation | PU insulation |
| Surface finish | Polished |
| Cleaning system | CIP optional |
| Voltage | Customized |
Capacity & Output
• Tank capacity: 50L – 1000L per unit
• Dual-tank total capacity: up to 2000L
• Alcohol output per cycle: 10L – 300L
• Daily production: 50L – 1000L
• Suitable for: small to medium distilleries
Main Features
• Dual-Tank Continuous Operation Design
The double tank configuration allows alternating or parallel operation, significantly reducing downtime between batches. While one tank is distilling, the other can be filled or cleaned, maximizing productivity and ensuring continuous alcohol production.
• High-Efficiency Distillation Performance
Optimized heating and vapor flow design improve distillation efficiency, ensuring faster processing time, higher alcohol recovery rates, and consistent output quality across every batch.
• SS304 Stainless Steel Construction
Manufactured with high-grade SS304 stainless steel, the equipment offers excellent corrosion resistance, hygienic operation, and long service life, making it suitable for food-grade and industrial applications.
• Flexible Operation Modes
Supports batch, alternating, and semi-continuous distillation processes. Operators can adjust the system according to production requirements, improving adaptability for different alcohol types and production scales.
• Stable Temperature Control System
Equipped with precise temperature monitoring and control mechanisms to ensure stable distillation conditions, which is critical for maintaining consistent alcohol quality and preventing process fluctuations.
• Optional Copper Components for Flavor Enhancement
Copper parts can be integrated to enhance catalytic reactions, effectively removing sulfur compounds and improving aroma, especially for premium spirits such as whiskey and brandy.
• Energy-Efficient Heating System
Optimized thermal design reduces heat loss and improves energy utilization, lowering operational costs while maintaining high production efficiency.
• Compact and Integrated System Design
The dual-tank structure is engineered to maximize capacity without significantly increasing footprint, making it suitable for facilities with limited space.
• Easy Cleaning and Maintenance
Smooth internal surfaces and optional CIP system allow quick cleaning and maintenance, reducing downtime and ensuring hygienic production conditions.
Engineering Advantages
• Alternating tank operation increases productivity.
• Efficient heat transfer improves energy usage.
• Stable process ensures consistent product quality.
• High-quality materials ensure long service life.
• Simplified maintenance reduces operational complexity.
Application Scenarios
• Craft distilleries aiming to increase production efficiency without expanding equipment footprint.
• Commercial distilleries requiring stable and continuous alcohol production.
• Startup distilleries needing flexible and scalable systems.
• Beverage companies integrating distillation into production lines.
• Pilot production setups for testing continuous distillation processes.
Industry Applications
• Distillery industry for whiskey, vodka, rum, and gin production.
• Alcohol production facilities requiring efficient processing.
• Beverage manufacturing industry.
• Fermentation and food processing industries.
• Small industrial alcohol production plants.
FAQ
What is the advantage of a double tank distillation system compared to a single tank?
A double tank system allows continuous or alternating operation, reducing downtime between batches and significantly increasing overall production efficiency.
Can both tanks operate at the same time?
Yes, the two tanks can operate independently or simultaneously, depending on production requirements and system configuration.
What types of alcohol can this equipment produce?
It is suitable for producing whiskey, rum, gin, vodka, brandy, and other distilled spirits, as well as industrial alcohol.
Is this system suitable for commercial distilleries?
Yes, it is designed for both small and medium commercial distilleries looking to improve production efficiency.
Can the equipment be customized?
Yes, we offer full customization including tank capacity, heating methods, control systems, and optional copper components.
What heating options are available?
Electric, steam, and gas heating systems are available to suit different facility requirements and energy sources.
Does the system support automation?
Yes, PLC automatic control systems can be integrated for precise process control and reduced labor requirements.
How does SS304 material benefit the system?
SS304 provides corrosion resistance, food-grade hygiene, and durability, ensuring long-term reliable operation.
Is the equipment energy efficient?
Yes, optimized heat transfer and system design significantly reduce energy consumption compared to traditional systems.
How easy is maintenance and cleaning?
The system is designed for easy cleaning with smooth internal surfaces and optional CIP systems, minimizing maintenance effort.
Contact us to get your quotation now.
Get in touch with our engineering team.
Related products
-
Distillery Equipment, Distillery System, Food & Beverage Processing Equipment
200L 500L 1000L Gin Distillation Equipment Whiskey Distiller Red Copper Distiller Moonshine Distiller
 Distillery Equipment, Distillery System, Food & Beverage Processing Equipment
200L 500L 1000L Gin Distillation Equipment Whiskey Distiller Red Copper Distiller Moonshine Distiller
Product name: Whiskey/Gin distiller
Material: 304 stainless steel/red copper
Shape: tower distiller
Size: 200L-5000L
More details are subject to negotiation, contact the supplier now for more details.SKU: n/a -
Distillery Equipment, Distillery System
500L Red Copper Stainless Steel Wine Gin Whiskey Still Pot Multifunctional Distillery pot Distillation Equipment
Distillery Equipment, Distillery System500L Red Copper Stainless Steel Wine Gin Whiskey Still Pot Multifunctional Distillery pot Distillation Equipment
Advantages of distillation equipment
A: Flanging welding technology is adopted at the welding position of distillation equipment to ensure no leakage of distillation equipment.
B: The distillation pot is divided into single layer, double layer and three layers. The three-layer distillation pot is jacketed for heating. The bottom and surrounding of the distillation pot are heated at the same time, which has high heating effect and energy-saving effect.
C: The split condenser and condenser are cooled by tubes. There are many tubes inside, with large heat exchange area and high cooling effect.SKU: n/a -
Distillery Equipment, Distillery System
500L Hot sales Alcohol Distillation Equipment Machine For Whisky Rum Gin Vodka Brandy Spirit Distiller Alcohol Distiller Factory
Distillery Equipment, Distillery System500L Hot sales Alcohol Distillation Equipment Machine For Whisky Rum Gin Vodka Brandy Spirit Distiller Alcohol Distiller Factory
Applicable Industries:Hotels, Garment Shops, Building Material Shops, Machinery Repair Shops, Manufacturing Plant, Food & Beverage Factory, Farms, Restaurant, Home Use, Retail, Food Shop, Printing Shops, Construction works , Energy & Mining, Advertising Company
SKU: n/a