15000L Distillery Equipment Manufacturer for Commercial Spirits
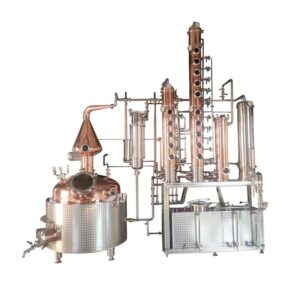
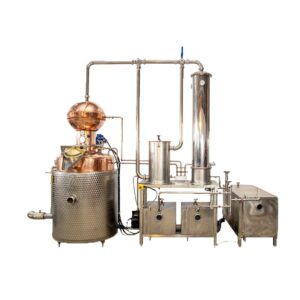
15000L distillery equipment designed for commercial and industrial spirits production, delivering high-capacity output and stable long-term performance. This system integrates advanced distillation technology with efficient heat transfer and precise process control to ensure consistent product quality. Ideal for whisky, vodka, gin, and rum production, it offers scalable configuration and turnkey solutions for large distillery projects and expansion plans.
Compare
15000L Distillery Equipment Product Introduction
As a professional distillery equipment manufacturer, we provide high-capacity 15000L distillation systems designed for commercial spirits production and industrial-scale operations. This system is engineered to deliver stable performance, high output, and consistent product quality, making it ideal for large distilleries and beverage production facilities.
The 15000L distillery equipment integrates advanced distillation technology with efficient heat transfer and precise process control. It is suitable for producing whisky, vodka, gin, rum, and other spirits at scale. We also provide complete turnkey distillery solutions including fermentation, distillation, storage, and auxiliary systems to support your full production line from raw materials to finished products.
System Overview
• Large-capacity 15000L distillation system designed for continuous and high-volume production
• Supports pot still, hybrid, or column distillation configurations based on product requirements
• Integrated heating, distillation, condensation, and control systems
• Suitable for industrial distilleries and large-scale spirits production plants
• Modular structure enables system expansion and process optimization
• Designed for long-term stable operation with high efficiency
Production Process Description
• Raw materials such as grains, molasses, or fruits are fermented into alcohol wash
• Fermented liquid is transferred into the distillation system
• Controlled heating vaporizes alcohol and volatile compounds
• Multi-stage separation ensures purification and concentration of alcohol
• Condenser converts vapor into liquid distillate
• Distillate is separated into heads, hearts, and tails
• Final product is transferred to storage or aging systems
Working Principle
• The system operates through controlled heating and condensation to separate alcohol from water and impurities
• Large-scale distillation unit ensures stable vapor generation and efficient separation
• Column or hybrid structures improve alcohol purity and processing efficiency
• Reflux control allows precise adjustment of alcohol strength and flavor
• Cooling system ensures stable condensation and continuous operation
Why This System Is Designed This Way
• 15000L capacity supports high-volume commercial production
• Advanced distillation design improves efficiency and reduces energy consumption
• Modular system allows customization based on production needs
• High-quality materials ensure durability and hygiene
• Designed for long-term industrial operation and scalability
Technical Specifications
| Capacity | 15000L |
| Effective volume | 12000–14000L |
| Distillation type | Pot still / Hybrid / Column |
| Material | Copper + SS304 / Optional SS316 |
| Heating method | Steam / Gas |
| Steam consumption | 300–800 kg/h |
| Distillation cycle time | 6–12 hours |
| Output capacity | 1500–5000L per batch |
| Alcohol concentration | 40–96% adjustable |
| Column type | Plate / Packed |
| Plate quantity | 10–30 plates optional |
| Condenser type | Shell & tube |
| Cooling system | Water-cooled |
| Cooling water consumption | 15–50 m³/h |
| Control system | Semi-auto / PLC |
| Power supply | 380V / 415V |
| Installation area | 150–400 m² |
Note:All configurations can be customized based on production capacity, spirit type, and plant requirements
Industry Applications
• Large commercial distilleries producing whisky, vodka, gin, and rum, requiring high output, consistent product quality, and stable long-term operation for regional and global distribution
• Industrial alcohol production plants manufacturing neutral spirits or base alcohol for beverage blending, where efficiency, purity, and production scale are critical
• Beverage companies and investment projects building new distillery facilities, requiring complete turnkey systems for full-scale spirits production
Solution Composition
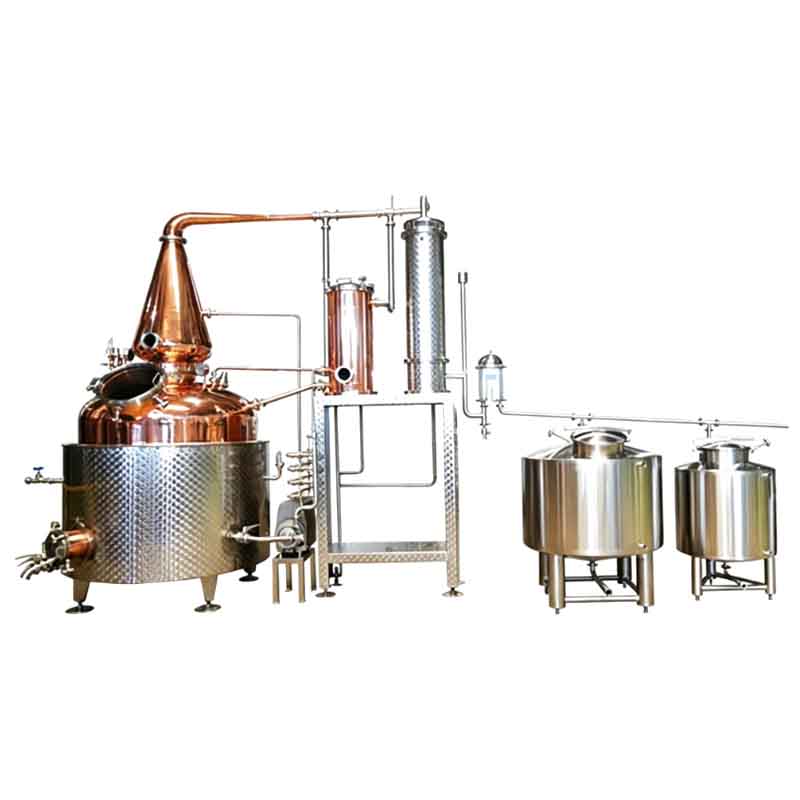
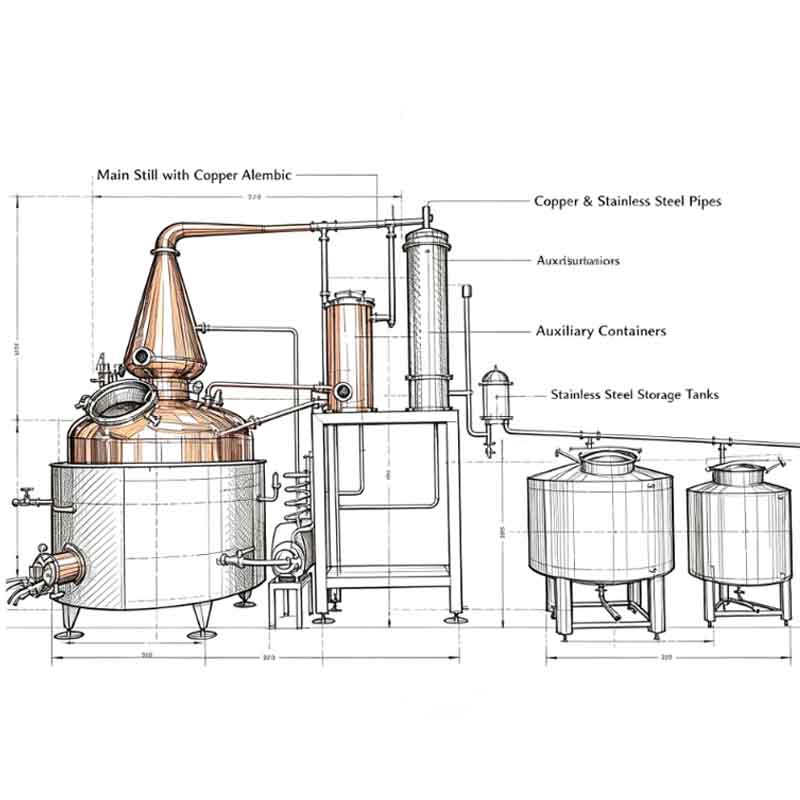
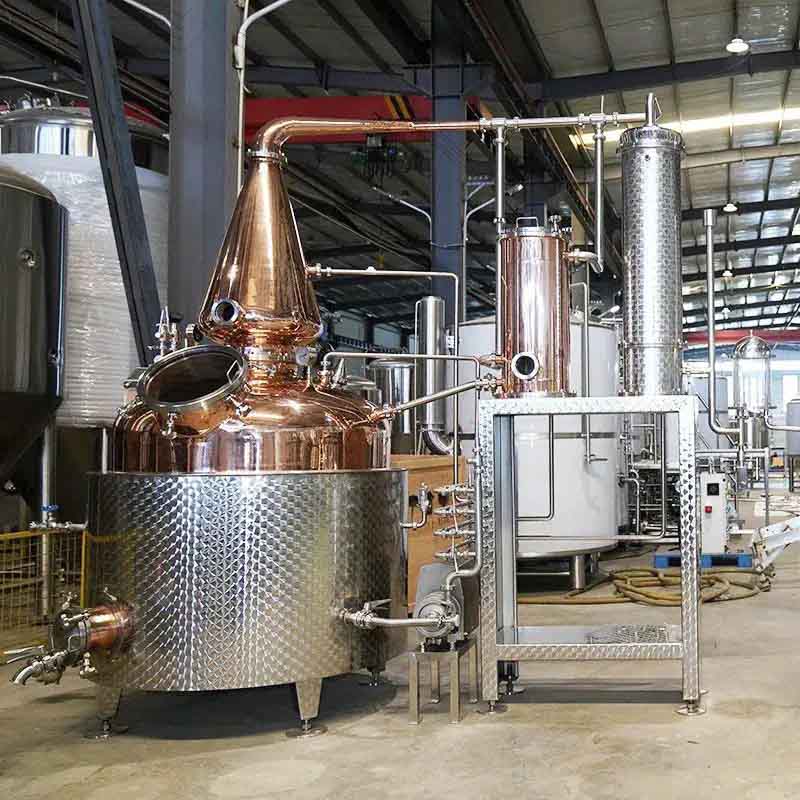
• Complete distillation system including large-capacity pot still or hybrid distillation unit, condenser, and reflux control system, forming the core of the alcohol production process
• Integrated auxiliary systems such as fermentation tanks, storage tanks, pipeline networks, heating systems, cooling systems, and control systems, ensuring efficient, hygienic, and continuous operation across the entire production line
Main Features
• 15000L large capacity suitable for industrial and commercial production
• High-efficiency distillation system with stable performance
• Flexible configuration for different spirits production
• Advanced heat transfer system for energy efficiency
• Durable construction with long service life
• Modular design for easy expansion
Key Engineering Advantages
• Large-scale system design ensures high productivity and stable output
• Multi-stage separation improves alcohol purity and consistency
• Optimized heat exchange reduces operational cost
• Advanced control system improves process stability
• Industrial-grade materials ensure durability and reliability
Application Scenarios
• Large commercial distilleries producing whisky, vodka, gin, rum, and other spirits at scale, where high production capacity, stable operation, and consistent product quality are critical for regional and international distribution
• Industrial alcohol production plants manufacturing neutral spirits or base alcohol for beverage blending, requiring continuous operation, high efficiency, and precise control of alcohol purity
• New distillery investment projects building full-scale production facilities, where a complete and reliable distillation system is needed to support long-term commercial operation and future capacity expansion
• Existing distilleries upgrading from smaller or outdated equipment to large-capacity systems in order to increase output, improve energy efficiency, and meet growing market demand
• Beverage companies entering large-scale spirits production, requiring integrated and scalable distillation solutions that can support multiple product types and production lines
• Export-oriented alcohol production facilities that require standardized, high-quality output and stable system performance for international markets
Why Choose This Machine
• As a direct manufacturer, we provide complete customization based on your production capacity, spirit type, and plant layout, ensuring the system perfectly matches your project requirements
• The 15000L large-capacity design significantly increases production efficiency and reduces unit production cost, making it ideal for commercial and industrial applications
• Advanced distillation technology ensures high alcohol purity and consistent product quality, helping you meet strict market and regulatory standards
• Optimized heat transfer and energy-efficient design reduce operating costs and improve long-term profitability
• Modular system structure allows easy installation, maintenance, and future expansion as your production demand grows
• High-quality materials such as stainless steel and copper ensure durability, corrosion resistance, and long service life in continuous industrial operation
• Integrated control system improves process stability, reduces manual operation, and enhances overall production efficiency
• Strong engineering support including system design, layout planning, and technical consultation ensures smooth project execution
FAQ
What spirits can be produced with this equipment?
Whisky, gin, vodka, rum, and other commercial spirits.
Can the system be customized?
Yes, configuration and capacity can be customized.
Is this suitable for industrial production?
Yes, it is designed for large-scale commercial and industrial operations.
Do you provide complete systems?
Yes, we provide full turnkey distillery solutions.
Contact us to get your quotation now.
Get in touch with our engineering team.
Related products
-
Distillery Equipment, Distillery System
Copper Distillery Equipment 1000L Pot Columns for Gin Vodka Whisky Brandy Rum
 Distillery Equipment, Distillery System
Copper Distillery Equipment 1000L Pot Columns for Gin Vodka Whisky Brandy Rum
We can customize stills according to your needs, with any size boiler or column diameter.
The columns & condensers can be made with copper or stainless steel according to your needs.
This still is versatile and multi-functional, great for stripping, Gin, Rum, Brandy, Moonshine, Vodka and Whiskey.SKU: n/a -
Distillery Equipment, Distillery System
1000Liter Distillery Equipment Rum Whisky Still Alcohol Distillation Machinery
Distillery Equipment, Distillery System1000Liter Distillery Equipment Rum Whisky Still Alcohol Distillation Machinery
Hybrid pot stills can be built either of copper or stainless steel. When built from stainless steel, the bottom and side shell of the pot are made of stainless, while the top of the pot is built from copper and welded together.
The Hybrid pot still can be build with various head designs, depending on the spirits being produced. The tray quntity in the rectification column is dependent on the desired ABV of the final distillate.
SKU: n/a -
Distillery Equipment, Distillery System
1000L Commercial Distillery Equipment Still Gin Distillation Machine
Distillery Equipment, Distillery System1000L Commercial Distillery Equipment Still Gin Distillation Machine
Commercial Distillery Equipment Components:
Still pot
Helmet
Distillation columns(optional)
Dephlegmator
Gin basket
Condenser
Parrot out mouth
Storage tank(Head heart tail)
Frame(table or tank)
CIP cleaning system
Electric control box
Steam generator FOR Steam heating.SKU: n/a