
2000 Gallon Hybrid Pot Still Manufacturer for Commercial Distillery
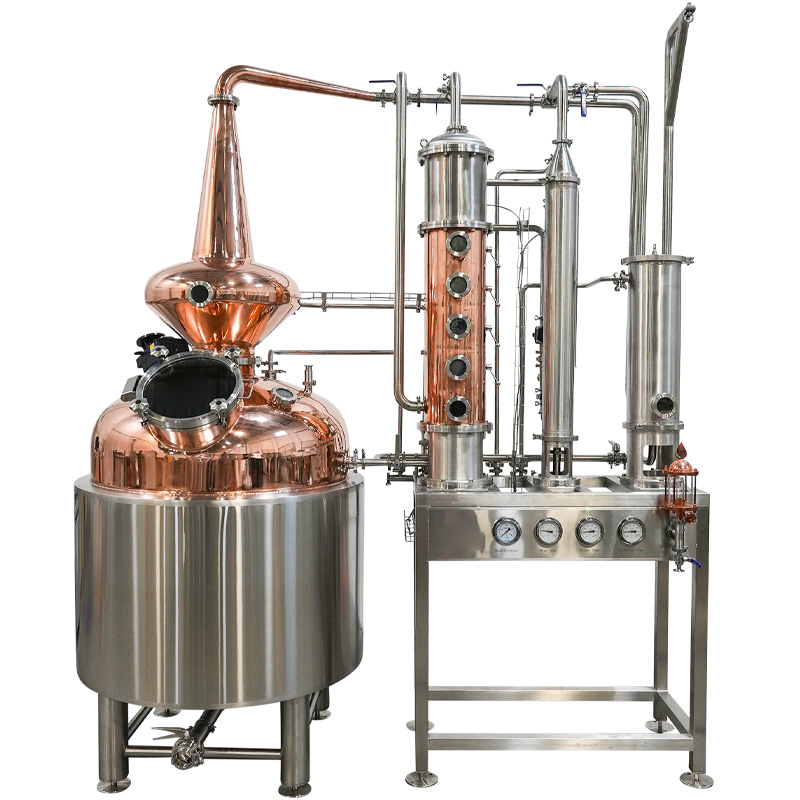
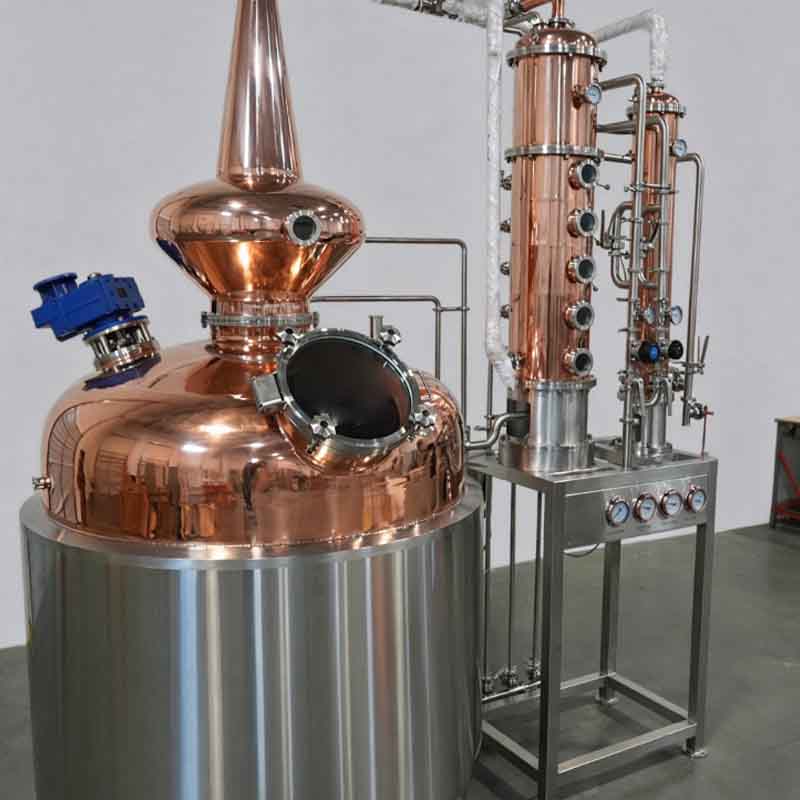
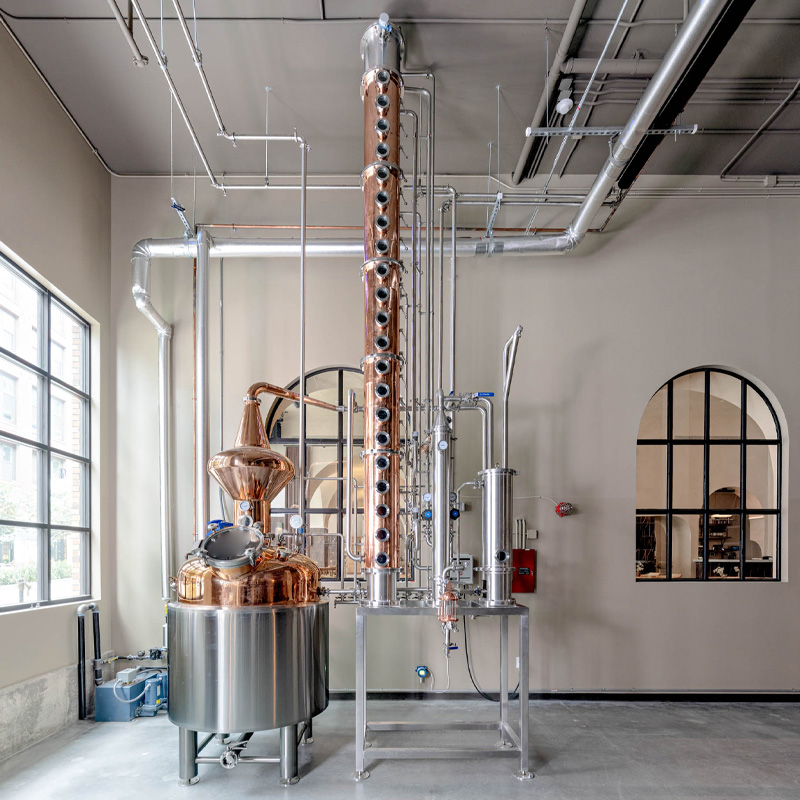
2000 gallon hybrid pot still designed for commercial distilleries producing premium spirits. Combining pot still and column distillation, it offers precise control over flavor and alcohol purity. Built with copper and stainless steel, the system ensures efficient operation, consistent performance, and flexible configuration for whisky, gin, vodka, and other spirits production.
Compare
2000 Gallon Hybrid Pot Still Product Introduction
As a professional hybrid pot still manufacturer, we provide high-performance 2000 gallon distillation systems designed for commercial distilleries producing premium spirits. This hybrid system combines the traditional pot still with a rectification column, allowing producers to achieve both rich flavor profiles and high alcohol purity in a single integrated unit.
The 2000 gallon hybrid pot still is ideal for distilleries producing whisky, gin, vodka, rum, and other craft or premium spirits. It is engineered to deliver precise temperature control, stable distillation performance, and flexible operation. We also provide complete distillery system integration including fermentation, distillation, and storage solutions to support your full production line.
System Overview
• The hybrid pot still combines pot still and column still functions in one system
• Designed for both flavor-focused batch distillation and higher-purity rectification
• Includes boiler, column section, condenser, and spirit collection system
• Suitable for medium to large-scale commercial distillery operations
• Supports multiple spirit styles with adjustable reflux and separation control
• Built with copper and stainless steel options for optimal performance
• Compatible with manual or PLC automation systems
Production Process Description
• Fermented mash or wash is transferred into the still
• Controlled heating vaporizes alcohol and volatile compounds
• Vapor rises through the column where separation and purification occur
• Reflux process improves alcohol concentration and removes unwanted components
• Vapor enters condenser and is converted into liquid distillate
• Distillate is separated into heads, hearts, and tails
• Desired spirit is collected and transferred for storage or aging
Working Principle
• The hybrid pot still operates based on the difference in boiling points between ethanol and water, allowing controlled vaporization and separation
• The pot section enhances flavor retention by preserving aromatic compounds
• The column section increases purity by providing multiple stages of rectification
• Adjustable reflux allows precise control over alcohol strength and flavor profile
• The condenser converts vapor into liquid while maintaining product integrity
• This combination allows distillers to switch between traditional and modern distillation styles
Why This System Is Designed This Way
• Hybrid design balances flavor complexity and alcohol purity
• Column section improves efficiency compared to traditional pot stills
• Copper contact enhances removal of sulfur compounds and improves taste
• Modular structure allows flexible configuration and future expansion
• Designed for consistent performance in commercial production
• Supports multiple spirit recipes with one system
Technical Specifications
| Total capacity | 2000 gallon (≈7500L) |
| Effective working volume | 1500–1800 gallon |
| Distillation type | Hybrid (Pot + Column) |
| Material | Copper + SS304 / Optional SS316 |
| Column type | Plate / Packed column |
| Plate quantity | 6–20 plates optional |
| Heating method | Steam / Electric / Gas |
| Steam consumption | 200–400 kg/h |
| Electric heating power | 80–200 kW |
| Operating temperature | 78–100°C |
| Distillation time | 6–12 hours per batch |
| Output capacity | 500–1500L per batch |
| Alcohol concentration | 40–96% adjustable |
| Condenser type | Shell & tube |
| Cooling system | Water-cooled |
| Cooling water consumption | 8–20 m³/h |
| Reflux control | Adjustable |
| Control system | Manual / Semi-auto / PLC |
| Safety system | Pressure relief valve |
| Power supply | 380V / 415V |
| Installation type | Modular |
| Service life | 10–20 years |
Note:All configurations can be customized based on raw materials, spirit type, and production requirements
Industry Applications
• Commercial distilleries producing whisky, gin, vodka, and rum
• Premium spirits manufacturers focusing on flavor quality
• Craft distilleries scaling production capacity
• Industrial alcohol production facilities
• Distillery expansion and upgrade projects
Solution Composition
• Fermentation system for mash or wash preparation
• Hybrid pot still system with column
• Condenser and cooling system
• Spirit collection and storage system
• Pipeline and valve system
• Control system for monitoring and automation
• Optional filtration and purification system
• Complete distillery production line integration
Main Features
• 2000 gallon capacity suitable for commercial distillery operations
• Hybrid design supports both flavor-rich and high-purity distillation
• Adjustable reflux provides precise control over alcohol strength
• High-efficiency condenser improves alcohol recovery
• Copper and stainless steel construction enhances performance and durability
• Flexible configuration for different spirit production requirements
• Reliable performance for continuous operation
• Modular design allows easy expansion
Key Engineering Advantages
• Hybrid design combining pot still and column distillation enables both flavor-rich spirits and high-purity alcohol production within one system, increasing production flexibility
• Multi-stage rectification column improves separation efficiency, allowing precise control of alcohol strength and removal of unwanted compounds
• Copper contact surfaces enhance sulfur removal and improve spirit aroma, which is essential for premium whisky and gin production
• Advanced reflux control system allows fine adjustment of distillation parameters, helping distillers achieve consistent product quality across batches
• Optimized heat transfer design improves energy efficiency and reduces operating costs in long-term commercial production
• High-efficiency condenser system ensures stable vapor condensation, improving alcohol recovery rate and minimizing product loss
• Modular system structure allows easy installation, maintenance, and future expansion based on production demand
• Robust construction with high-quality stainless steel and copper ensures durability and long service life under continuous industrial operation
Application Scenarios
• Commercial distilleries producing whisky, gin, vodka, and rum with consistent quality and scalable output
• Premium spirits producers focusing on flavor development, aroma control, and product differentiation
• Craft distilleries expanding production capacity while maintaining artisanal quality standards
• Multi-product distilleries requiring flexible equipment capable of switching between different spirit types
• Industrial alcohol production facilities requiring efficient and stable distillation systems
• Distillery investment projects building new production lines for regional or export markets
• Distillery expansion projects upgrading from traditional pot stills to hybrid systems for improved efficiency
• Contract distilling facilities producing spirits for multiple brands with varying specifications
• Beverage companies entering the spirits market and requiring reliable and scalable distillation solutions
Why Choose This Machine
• Direct manufacturer with strong customization capability
• Hybrid design offers flexibility and efficiency
• High-quality materials and strict quality control
• Reliable performance and long service life
• Strong engineering support and technical service
• Suitable for both new and expansion projects
• High return on investment for commercial production
FAQ
What is a hybrid pot still?
A hybrid pot still combines a traditional pot still with a column, allowing both flavor-rich and high-purity distillation.
What spirits can be produced?
Whisky, gin, vodka, rum, and other premium spirits.
Can the system be customized?
Yes, configuration, material, and control system can be customized.
Is this system suitable for commercial production?
Yes, it is designed for medium to large-scale distillery operations.
How is product quality controlled?
Through temperature control, reflux adjustment, and fraction separation.
Contact us to get your quotation now.
Get in touch with our engineering team.
Related products
-
Distillery Equipment, Distillery System
1000L Distillery Equipment Premium Commercial Copper Pot Still
 Distillery Equipment, Distillery System
1000L Distillery Equipment Premium Commercial Copper Pot Still
Fill capacity: 1000ltr
Shaped helmet: connected using stainless steel flanging without visible screws or gaskets inside or outside. with viewing glasses and thermometer.
Bubblecaps: new construction with increased copper surface and turbulent motion of the liquid. Free adjustable fluid level on distillation plates – flexible adjustment of alcohol content and aroma of distilled mash.
Including a pre-condenser in the head of the column (dephlegmator)SKU: n/a -
Distillery Equipment, Distillery System
Multi Function Make Machine 500L Stills Distillery Copper Distillation Equipment/ Gin /Vodka/Whisky Distiller/Distillery
Distillery Equipment, Distillery SystemMulti Function Make Machine 500L Stills Distillery Copper Distillation Equipment/ Gin /Vodka/Whisky Distiller/Distillery
Multi Function Make Machine 500L Stills Distillery Copper Distillation Equipment/ Gin /Vodka/Whisky Distiller/Distillery
Customized Commerce Distiller :Gin, vodka, whiskey, rum, brandy, tequila from 200L to 20,000L .Fast Delivery.20 years of manufacturing experience. Please Contact Us For The Offer!
Our equipment is as highly functional and efficient as it is aesthetically pleasing.SKU: n/a -
Distillery Equipment, Distillery System
Hot Sale 500L High Tower Distiller Liquor Brewing Equipment Ace spirit Distillation machine Vodka distillery equipment
Distillery Equipment, Distillery SystemHot Sale 500L High Tower Distiller Liquor Brewing Equipment Ace spirit Distillation machine Vodka distillery equipment
Our Factory Make Distillation Equipment,Beer Brewing Equipment Etc.
Export Equipment Capacity:200-5000L
Beer Brewing Equipment:Brew House, Mash Tun, Fermenter Tank, Beer Bright Tank, Water Tank etc.
Other Equipment:Storage Tank,CIP Cleaning Machine,other stainless steel customized Products.
Distillation Equipment:Include whiksy/Rum/Brandy/Gin/Vodka/Multi-spirit stills;Essential Oil DistillerSKU: n/a


