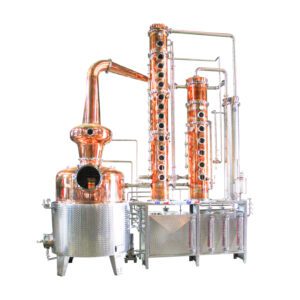
As a professional distillery equipment supplier, we provide high-quality 1000L distillation systems designed for craft spirits production and small to medium distillery operations. This equipment ensures stable distillation performance, precise temperature control, and efficient alcohol separation, helping producers achieve consistent spirit quality.
The 1000L distillery equipment is engineered for flexibility and scalability, making it suitable for producing whisky, vodka, gin, rum, and other spirits. It can be integrated into a complete distillery system including fermentation, distillation, and storage processes. We also provide complete distillery system integration including raw material processing, distillation, and storage solutions to support your full production line.
System Overview
· The 1000L distillery equipment is designed for batch distillation of alcoholic beverages
· Includes mash tank, fermentation tank, distillation still, condenser, and auxiliary systems
· Equipped with high-efficiency heating system for uniform temperature control
· Supports both pot still and column still configurations
· Integrated cooling system ensures efficient condensation of alcohol vapors
· Designed for manual or automated operation depending on requirements
· Suitable for continuous and stable craft spirits production
Production Process Description
· Raw materials such as grains, fruits, or molasses are prepared and fermented into alcohol wash
· The fermented liquid is transferred into the distillation still
· Heat is applied to vaporize alcohol at controlled temperature
· Alcohol vapors rise and pass through distillation column or head
· Vapors are condensed into liquid form through cooling system
· Distilled spirits are collected and separated into different fractions
· Final product is stored, aged, or processed further
Working Principle
· The system operates based on differences in boiling points between alcohol and water, allowing separation through controlled heating and condensation
· During heating, ethanol vaporizes at a lower temperature than water, enabling selective separation of alcohol components
· Vapor travels through the distillation column or head where impurities are separated and purified
· The condenser cools vapor into liquid, forming distilled spirits with higher alcohol concentration
· Fractional separation allows removal of unwanted components such as methanol and fusel oils
· Temperature and flow control ensure consistent distillation quality and repeatable production results
· The system is designed for efficient heat transfer and energy utilization, improving overall production efficiency
Why This System Is Designed This Way
· Optimized still design improves separation efficiency and product purity
· Controlled heating system ensures stable distillation performance
· Stainless steel construction provides hygiene and corrosion resistance
· Modular structure allows flexible configuration and expansion
· Efficient condenser design improves alcohol recovery rate
· Designed for both small-scale and commercial distillery production
Technical Specifications
| Total volume |
1000L |
| Material |
SS304 / Optional copper / SS316 |
| Inner surface finish |
≤0.6μm |
| Outer surface finish |
2B / Polished optional |
| Distillation type |
Pot still / Column still optional |
| Column configuration |
Tray / Packed column optional |
| Number of trays |
4–12 plates optional |
| Heating method |
Electric / Steam / Gas |
| Heating power (electric) |
24–60 kW |
| Steam consumption |
50–100 kg/h |
| Operating temperature |
78–100°C |
| Distillation time |
4–8 hours per batch |
| Alcohol recovery rate |
≥85% |
| Output capacity |
80–200L per batch (depending on raw material) |
| Alcohol concentration |
40–95% adjustable |
| Cooling system |
Water-cooled condenser |
| Cooling water consumption |
2–5 m³/h |
| Condenser type |
Shell & tube / Coil |
| Cooling temperature |
≤25°C |
| Control system |
Manual / Semi-auto / PLC optional |
| Temperature control |
Digital sensor + controller |
| Pressure condition |
Atmospheric pressure |
| Safety system |
Pressure relief valve |
| Agitator |
Optional |
| Manhole |
Top manway |
| CIP system |
Optional spray ball |
| Cleaning method |
Manual / CIP optional |
| Pipeline material |
Stainless steel sanitary pipe |
| Valve type |
Sanitary valve |
| Installation type |
Modular / Skid-mounted |
| Footprint area |
15–30 m² |
Note: All specifications can be customized based on raw material type, distillation process, and production requirements
Industry Applications
· Craft distilleries producing whisky, vodka, gin, rum, and specialty spirits
· Small to medium distillery operations scaling production capacity
· Beverage production facilities entering spirits manufacturing
· Pilot distillation systems for product development
· Distillery expansion projects increasing output
· Alcohol production for food, pharmaceutical, and industrial applications
· Regional distillery brands targeting consistent product quality
Solution Composition
· Fermentation system for alcohol production
· Distillation still system including boiler and column
· Condenser and cooling system for vapor condensation
· Storage tanks for raw and finished products
· Pump and pipeline system for liquid transfer
· Control system for temperature and process control
· Optional filtration and purification system
· Complete distillery production line integration
Main Features
· 1000L capacity ideal for craft spirits production
· High-efficiency distillation for stable alcohol separation
· Flexible configuration for different spirits production
· Stainless steel structure ensures hygiene and durability
· Precise temperature control improves product quality
· Energy-efficient design reduces operating cost
· Easy operation and maintenance
· Suitable for batch and semi-continuous production
· Modular design supports system expansion
· Reliable performance for long-term operation
Key Engineering Advantages
· Optimized distillation design ensures efficient separation and higher product purity, improving final spirit quality
· Advanced heating and cooling system provides stable temperature control, ensuring consistent and repeatable distillation results
· High-quality stainless steel construction enhances durability, corrosion resistance, and hygienic performance
· Flexible system configuration supports various distillation methods and different types of spirits production
· Efficient condenser design improves alcohol recovery and reduces energy loss during production
· Modular structure allows easy installation, maintenance, and integration into existing distillery setups
· Reliable system performance reduces downtime and ensures continuous production efficiency
· Proven design based on real distillery operations ensures stable and long-term use
Application Scenarios
· Craft distillery production lines producing premium spirits such as whisky, vodka, gin, and rum
· Small to medium distilleries expanding production capacity while maintaining product quality and flexibility
· New distillery projects requiring cost-effective and scalable equipment solutions
· Pilot distillation systems used for developing new recipes and testing production processes
· Beverage manufacturers entering the spirits production market
· Regional distilleries targeting consistent output and standardized product quality
· Distillery upgrade projects replacing outdated or inefficient equipment
· Industrial alcohol production facilities requiring controlled and efficient distillation processes
Why Choose This Machine
· Designed specifically for craft spirits production
· Stable performance with high distillation efficiency
· Flexible configuration for various production needs
· Competitive pricing with high cost-performance ratio
· Professional engineering support and customization
· Easy integration into complete distillery systems
· Reliable long-term operation
· Suitable for both new and expansion projects
With extensive experience in distillery equipment manufacturing, we provide reliable and efficient solutions for customers worldwide
FAQ
What is a 1000L distillery equipment used for?
It is used for distilling alcohol from fermented liquids to produce spirits such as whisky, vodka, gin, and rum.
What types of spirits can be produced?
The system supports a wide range of spirits including whisky, vodka, gin, rum, and other distilled beverages.
Can the equipment be customized?
Yes, material, heating method, and configuration can be customized based on your requirements.
What is the difference between pot still and column still?
Pot still is used for batch distillation with richer flavor, while column still allows continuous distillation with higher purity.
Do you provide complete distillery solutions?
Yes, we provide full system integration including fermentation, distillation, and storage.
What is the delivery time?
Typically 20–40 working days depending on customization.
Contact us to get your quotation now.
Get in touch with our engineering team.

 Distillery Equipment, Distillery System