6000L Distillery Equipment Supplier for Premium Spirits
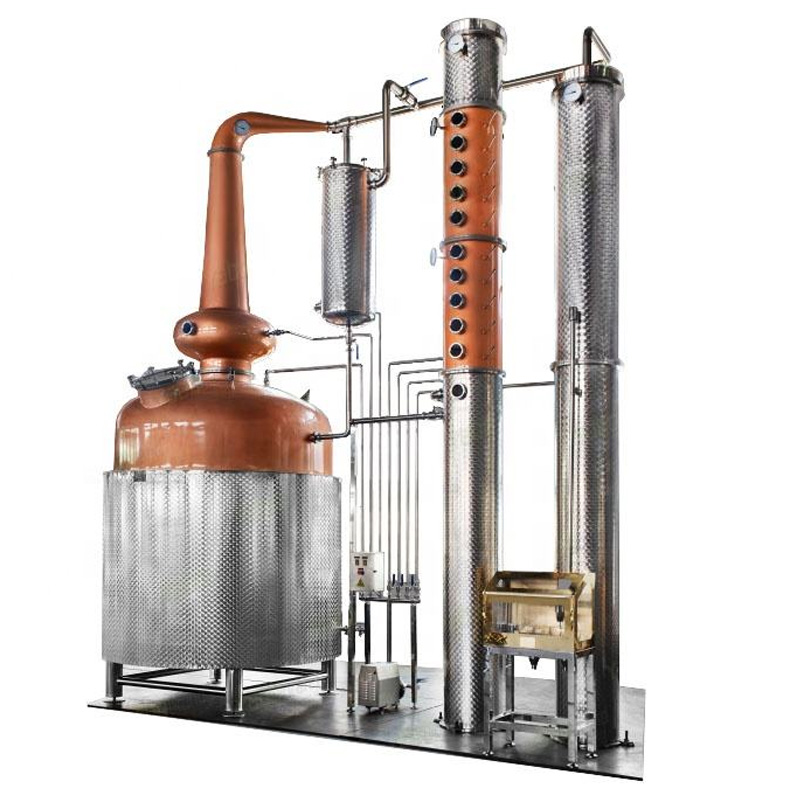
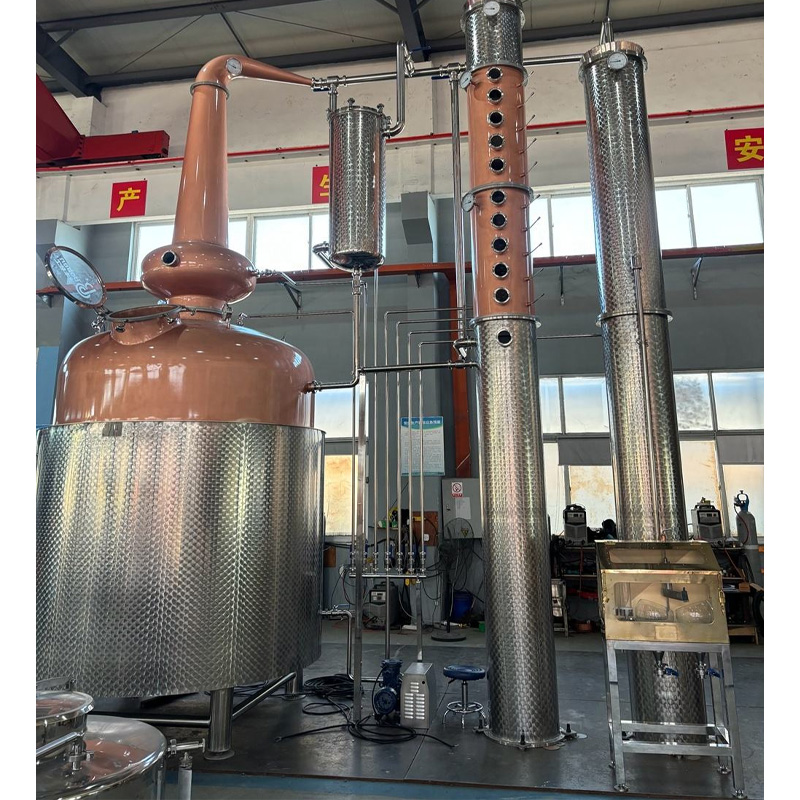
6000L distillery equipment designed for commercial and premium spirits production, integrating fermentation, distillation, and cooling systems to ensure high efficiency, stable operation, and consistent product quality across large-scale industrial applications.
Compare
6000L Distillery Equipment Product Introduction
As a professional distillery equipment supplier, we provide high-capacity 6000L distillation systems designed for commercial and premium spirits production. This system is engineered for large-scale operations, delivering stable distillation performance, efficient alcohol separation, and consistent product quality.
The 6000L distillery equipment is ideal for commercial distilleries producing whisky, gin, vodka, rum, and other premium spirits. It is designed to maintain flavor integrity while improving production efficiency and output capacity. We also provide complete distillery system integration including fermentation, distillation, and storage solutions to support your full production line.
System Overview
· The 6000L distillery system is designed for large-scale commercial spirits production
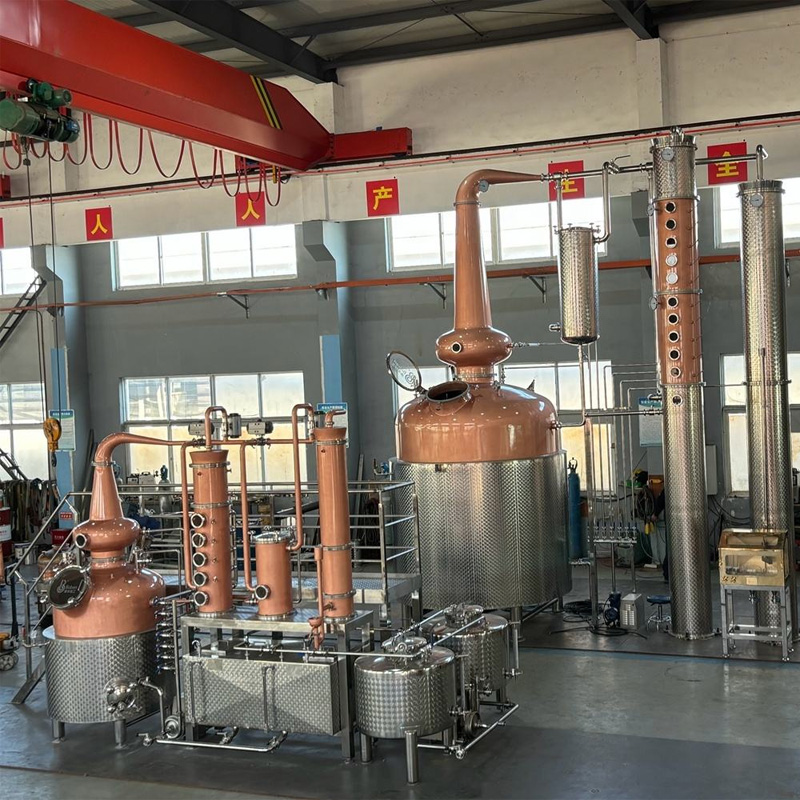
· Includes distillation still, column system (optional), condenser, and auxiliary units
· Supports both pot still and column distillation for flexible production
· Designed for high output capacity with stable operation
· Equipped with efficient heating system for uniform temperature control
· Advanced condenser ensures high alcohol recovery rate
· Suitable for automated control and continuous production environments
Production Process Description
· Raw materials such as grains, fruits, or molasses are fermented into alcohol wash
· Fermented liquid is transferred into the distillation still
· Heating system vaporizes alcohol and volatile compounds
· Vapor travels through the column or head for purification
· Condenser cools vapor into liquid form
· Distillate is separated into heads, hearts, and tails
· Final spirit is collected and transferred for storage or aging
Working Principle
· The system operates based on the difference in boiling points between ethanol and water, allowing controlled separation through heating and condensation
· Ethanol vaporizes at approximately 78°C, lower than water, enabling selective extraction of alcohol and aromatic compounds
· Vapor rises through the column or still head, where reflux improves separation efficiency
· Condenser converts vapor into liquid while maintaining product purity
· Fractional separation allows removal of undesirable components and retention of flavor compounds
· Temperature and reflux control ensure stable and repeatable production
Why This System Is Designed This Way
· Designed for large-scale commercial production with high output efficiency
· Optimized structure balances alcohol purity and flavor retention
· Modular design allows flexible configuration and future expansion
· Efficient heat transfer reduces energy consumption and operating cost
· High-quality materials ensure durability and hygienic production
· Suitable for long-term industrial distillery operation
Technical Specifications
| Total volume | 6000L |
| Material | SS304 / Copper optional / SS316 optional |
| Distillation type | Pot still / Column still |
| Column configuration | Tray / Packed column |
| Tray quantity | 8–20 plates optional |
| Heating method | Steam / Gas / Electric |
| Heating power | 80–180 kW |
| Steam consumption | 150–300 kg/h |
| Operating temperature | 78–100°C |
| Distillation time | 6–12 hours per batch |
| Output capacity | 400–1200L per batch |
| Alcohol concentration | 40–95% adjustable |
| Cooling system | Water-cooled condenser |
| Cooling water consumption | 6–15 m³/h |
| Control system | Semi-auto / PLC |
| Safety system | Pressure relief valve |
| Power supply | 380V / 415V |
| Installation type | Modular |
Note:All specifications can be customized based on raw materials, production scale, and process requirements
Industry Applications
· Large Commercial Distilleries Producing Premium Spirits
Designed for large-scale distilleries focused on high-end spirits production, supporting continuous fermentation and precision distillation processes to ensure consistent flavor profiles, high purity, and stable output for premium market positioning.
· Industrial Alcohol Production Plants
Widely used in industrial ethanol and alcohol manufacturing facilities, enabling high-efficiency distillation, energy-saving operation, and large-volume throughput for applications such as fuel alcohol, food-grade alcohol, and pharmaceutical-grade ethanol.
· Whiskey, Gin, Vodka, Rum Production Facilities
Suitable for diverse spirits production including whiskey, gin, vodka, and rum, with flexible configuration options for different distillation methods such as pot still and column still systems, ensuring optimal extraction of aroma compounds and product quality.
· High-Capacity Distillery Expansion Projects
Ideal for distillery capacity expansion and modernization projects, providing scalable solutions that integrate seamlessly with existing production lines, improving automation levels, production efficiency, and overall plant output.
· Export-Oriented Spirits Manufacturing
Engineered for export-focused manufacturers requiring international quality standards, consistent batch control, and compliance with global food and beverage processing regulations, ensuring competitiveness in overseas markets.
Solution Composition
· Fermentation System for Alcohol Wash Production
Includes fermentation tanks, agitation and temperature control modules, designed to ensure stable yeast activity and efficient sugar conversion, providing a consistent and high-quality alcohol base for downstream distillation.
· Distillation System Including Pot Still and Column Still
Core distillation unit supporting both traditional pot still and continuous column distillation, enabling flexible production of flavor-rich spirits or high-purity alcohol with precise separation control.
· Condenser and Cooling System
Equipped with high-efficiency condensers and optimized cooling circulation systems to rapidly condense alcohol vapor, improve recovery rates, and maintain stable system pressure during operation.
· Storage Tanks for Raw and Finished Spirits
Food-grade storage tanks designed for both intermediate alcohol and final spirits, ensuring safe storage, contamination prevention, and preservation of product quality and aroma.
· Pipeline and Valve System
Integrated sanitary piping network with precision valves for controlled liquid transfer, minimizing leakage, ensuring hygienic operation, and supporting automated production flow.
· Control System for Process Monitoring
Advanced PLC-based control system with real-time monitoring of temperature, pressure, and flow rate, enabling precise process control, automation, and reduced labor dependency.
Main Features
· 6000L Large Capacity for High-Output Production
Engineered for large-scale commercial distilleries, delivering high batch volume and continuous production capability to meet industrial output demands.
· Supports Both Flavor-Focused and High-Purity Distillation
Flexible design accommodates different distillation objectives, from aroma-rich traditional spirits to high-purity neutral alcohol production.
· High-Efficiency Heating System
Optimized heating methods (steam or electric) ensure uniform heat distribution, faster distillation cycles, and improved energy efficiency.
· Advanced Condenser Design for Maximum Alcohol Recovery
Enhanced heat exchange performance increases condensation efficiency, reduces alcohol loss, and improves overall yield.
· Durable Stainless Steel and Copper Construction
Combines corrosion-resistant stainless steel with copper components to enhance durability while improving sulfur compound removal and flavor refinement.
· Flexible Configuration for Multiple Production Needs
Customizable system layout and modular components allow adaptation to different raw materials, recipes, and production scales.
Key Engineering Advantages
· Optimized distillation design improves separation efficiency and product quality
· High-capacity system reduces production time and increases output
· Efficient heat exchange system reduces energy consumption
· Advanced reflux control improves alcohol purity and consistency
· Strong structural design ensures long-term durability
· Proven industrial design supports stable large-scale production
Application Scenarios
· Large-scale commercial distilleries focusing on premium spirits production
· Industrial plants producing high volumes of alcohol
· Distillery expansion projects increasing production capacity
· Export-oriented production facilities
· High-end spirits manufacturing plants
Why Choose This Machine
· Designed for large-scale commercial distillery operations
· High efficiency and stable performance
· Flexible customization options
· Strong engineering support
· Reliable long-term operation
· High return on investment
FAQ
What types of spirits can be produced?
Whisky, gin, vodka, rum, and other premium spirits.
Is this system suitable for large-scale production?
Yes, it is designed specifically for high-capacity commercial distilleries.
Can the system be customized?
Yes, materials, configuration, and control systems can be customized.
What is the difference between pot still and column still?
Pot still focuses on flavor, while column still improves purity and efficiency.
What is the delivery time?
Typically 30–60 working days depending on customization.
Contact us to get your quotation now.
Get in touch with our engineering team.
Related products
-
Distillery Equipment, Distillery System, Food & Beverage Processing Equipment
200L 500L 1000L Gin Distillation Equipment Whiskey Distiller Red Copper Distiller Moonshine Distiller
 Distillery Equipment, Distillery System, Food & Beverage Processing Equipment
200L 500L 1000L Gin Distillation Equipment Whiskey Distiller Red Copper Distiller Moonshine Distiller
Product name: Whiskey/Gin distiller
Material: 304 stainless steel/red copper
Shape: tower distiller
Size: 200L-5000L
More details are subject to negotiation, contact the supplier now for more details.SKU: n/a -
Distillery Equipment, Distillery System
Copper Distillery Equipment 1000L Pot Columns for Gin Vodka Whisky Brandy Rum
Distillery Equipment, Distillery SystemCopper Distillery Equipment 1000L Pot Columns for Gin Vodka Whisky Brandy Rum
We can customize stills according to your needs, with any size boiler or column diameter.
The columns & condensers can be made with copper or stainless steel according to your needs.
This still is versatile and multi-functional, great for stripping, Gin, Rum, Brandy, Moonshine, Vodka and Whiskey.SKU: n/a -
Distillery Equipment, Distillery System
Craft Distillery Equipment 1000L Commercial Whisky Vodka Copper Distiller
Distillery Equipment, Distillery SystemCraft Distillery Equipment 1000L Commercial Whisky Vodka Copper Distiller
Pot still sizes range from 500 litres to 2,000 litres (120 gallons to 500 gallons), can be constructed with stainless steel and/or copper, and usually offered in a hybrid-style pot still with a wide selection of heads, bypassable multi-tray rectification columns and gin basket complete with the condenser. Customized to suite your specific spirit range.
Pot Still
The pot still can be offered in a combination of stainless steel and copper construction or all copper construction
Heating options include steam jackets, and electric
Full CIP
Optional agitator
Optional glass manway
Optional vessel lightSKU: n/a