5–20 m/min Multi-Layer Mesh Belt Conveyor for Food Cooling
The Multi-Layer Mesh Belt Conveyor is designed for efficient long-distance material handling in fixed production environments. Featuring stainless steel mesh, plastic modular, chain rod, or chain plate belts, it supports high loading capacity and stable transport. Its self-supporting structure, sprocket-driven system, and modular design allow easy assembly, low maintenance, and smooth operation. Ideal for food, beverage, snack, and industrial production lines, it ensures high efficiency, low noise, and reliable continuous material flow.
Compare
Multi-Layer Mesh Belt Conveyor Product Introduction
The Multi-Layer Mesh Belt Conveyor is a versatile automated conveying system built for long-distance material transport in fixed production layouts. It uses high-strength belts including stainless steel mesh, plastic modular, chain rod, and chain plate options, capable of carrying heavy-duty products with high load and tensile strength. The self-supporting frame ensures stable operation without additional support, while sprocket-driven belts provide accurate tracking. This conveyor is easy to install, clean, and maintain, making it ideal for food, beverage, snack, frozen, and industrial product lines that require efficient, reliable, and hygienic material handling solutions.

Product Parameter Table
| Frame Material | Carbon /Gaivanzied Steel / SUS 304 |
| Belt Material | Carbon Steel/ SUS201 304 316 |
| Weight Capacity(kg) | 30-100 or Customized |
| Speed(m/min) | 5-20 or Customized |
| Power(W) | 90/220 or Customized |
| Conveyor/Belt Width | Customized |
| Adjustable Feet | Single/Double/Tripod Base |
| Guide Rail | Customized |
| Conveyor Height | Customized |

Main Features
-
High loading capacity belts allow safe transport of heavy-duty products across multi-layer conveyor systems.
-
Self-supporting frame design eliminates the need for extra structural supports, simplifying installation and maintenance.
-
Sprocket-driven mechanism ensures smooth operation with stable running and precise tracking of the conveyor belts.
-
Multiple belt options including stainless steel mesh, plastic module, chain rod, and chain plate for versatile applications.
-
Low maintenance and easy cleaning enable hygienic operation in food and industrial environments with minimal downtime.
-
Modular structure allows quick assembly, adaptability to new production layouts, and integration with existing systems.

Application Scenarios
-
Food and beverage: long-distance transport of baked goods, snacks, and packaged foods.
-
Frozen food: efficient handling of ice cream, seafood, and frozen products across multiple layers.
-
Industrial production: conveying heavy-duty components, metal parts, or packaged items.
-
Packaging and sorting lines: integration with automated systems for high throughput and precise flow.
-
Snack and confectionary: transport of chocolate, biscuits, or other delicate products without damage.

FAQ
Q1: What types of products can be conveyed?
A: Heavy-duty items, packaged foods, frozen products, snacks, metal parts, and industrial components.
Q2: Can it be used in food production environments?
A: Yes, it supports stainless steel and hygienic belt options suitable for food handling.
Q3: Is the conveyor easy to maintain?
A: Yes, modular design and sprocket-driven belts allow simple cleaning and low maintenance.
Q4: Can the conveyor handle multiple layers?
A: Yes, the system is designed for multi-layer material handling with stable operation.
Q5: Are there different belt types available?
A: Yes, stainless steel mesh, plastic modular, chain rod, and chain plate belts are all available.
Q6: Can it integrate with existing production lines?
A: Yes, the modular structure allows easy adaptation to existing layouts and automation systems.

Contact us to get your quotation now.
Get in touch with our engineering team.
Download full specification PDF.
Related products
-
Conveyors & Feeding Elevator
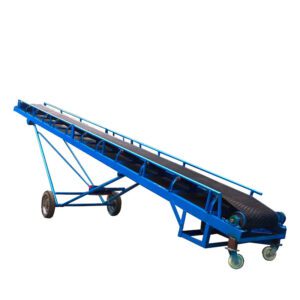
industrial mobile belt conveyor for coal/bulk material/sand gravel stone transporting
 Conveyors & Feeding Elevator
industrial mobile belt conveyor for coal/bulk material/sand gravel stone transporting
Our advantages on belt conveyor:
1).OEM service.
2).More than 30 years experience of conveying industry.Specialized in various conveyors(0-90 degree transportation),like Mobile Belt Conveyor,Fixed Belt Conveyor,Screw Conveyor,PVC Belt Conveyor,PVC(Rubber) Sidewall Belt Conveyor etc.
3).Delivery on time.
4).3% to 10% discounts for new customer(Based on the quantity.)
5).Professional engineer team help you to choose best model for your projectSKU: n/a -
Conveyors & Feeding Elevator
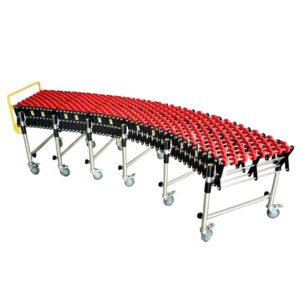
Gravity Expandable flexible roller conveyor for container unloading
* Flexible conveyors are exceptional for truck loading and unloading, retail stores, shipping areas, loading docks and plant floors.
* Portable, expandable conveyors allow you to quickly create a temporary conveyor line where you require it. Just extend and curve the conveyor to meet your needs.
* It makes skillful use of movement ,expansion and compaction so that floor space required can be reduced remarkably.
* It is self- tracking—cartons follow the twists and turns of the conveyor path without side rails or engineered curves.SKU: n/a -
Conveyors & Feeding Elevator
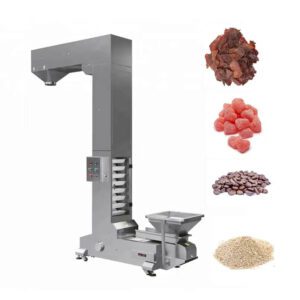
Industrial conveyor automatic z type conveyor bucket elevator for grain,snacks,nuts food grade conveyor
Conveyors & Feeding ElevatorIndustrial conveyor automatic z type conveyor bucket elevator for grain,snacks,nuts food grade conveyor
The conveyor is applicable for vertical lifting of granule material such as corn,jerry, snack, candy , nuts, plastic and chemical product, small hardware ,vegetable ,fruit and so on. For this machine, the bucket is driven by the chains to lift.
SKU: n/a -
Conveyors & Feeding Elevator
Gravity Flexible Expandable Plastic Skate Wheel Roller Conveyor
Gravity flexible expandable skate wheels conveyor is designed for handling of small-and medium-sized cartons/boxes. It use steel structure completely. The structure remains integrated when laying out according to complete expansion of single curve or composite curve remains integrated.
SKU: n/a